Live AI Dream Session, Vol. 3: Trustworthy AI in Practice with Sarath Kuravi and Dr. Shonraj Ballae • Nov 10 | 11:00 AM EST Reserve Your Seat Claim Free Seat

Reserve Your Seat

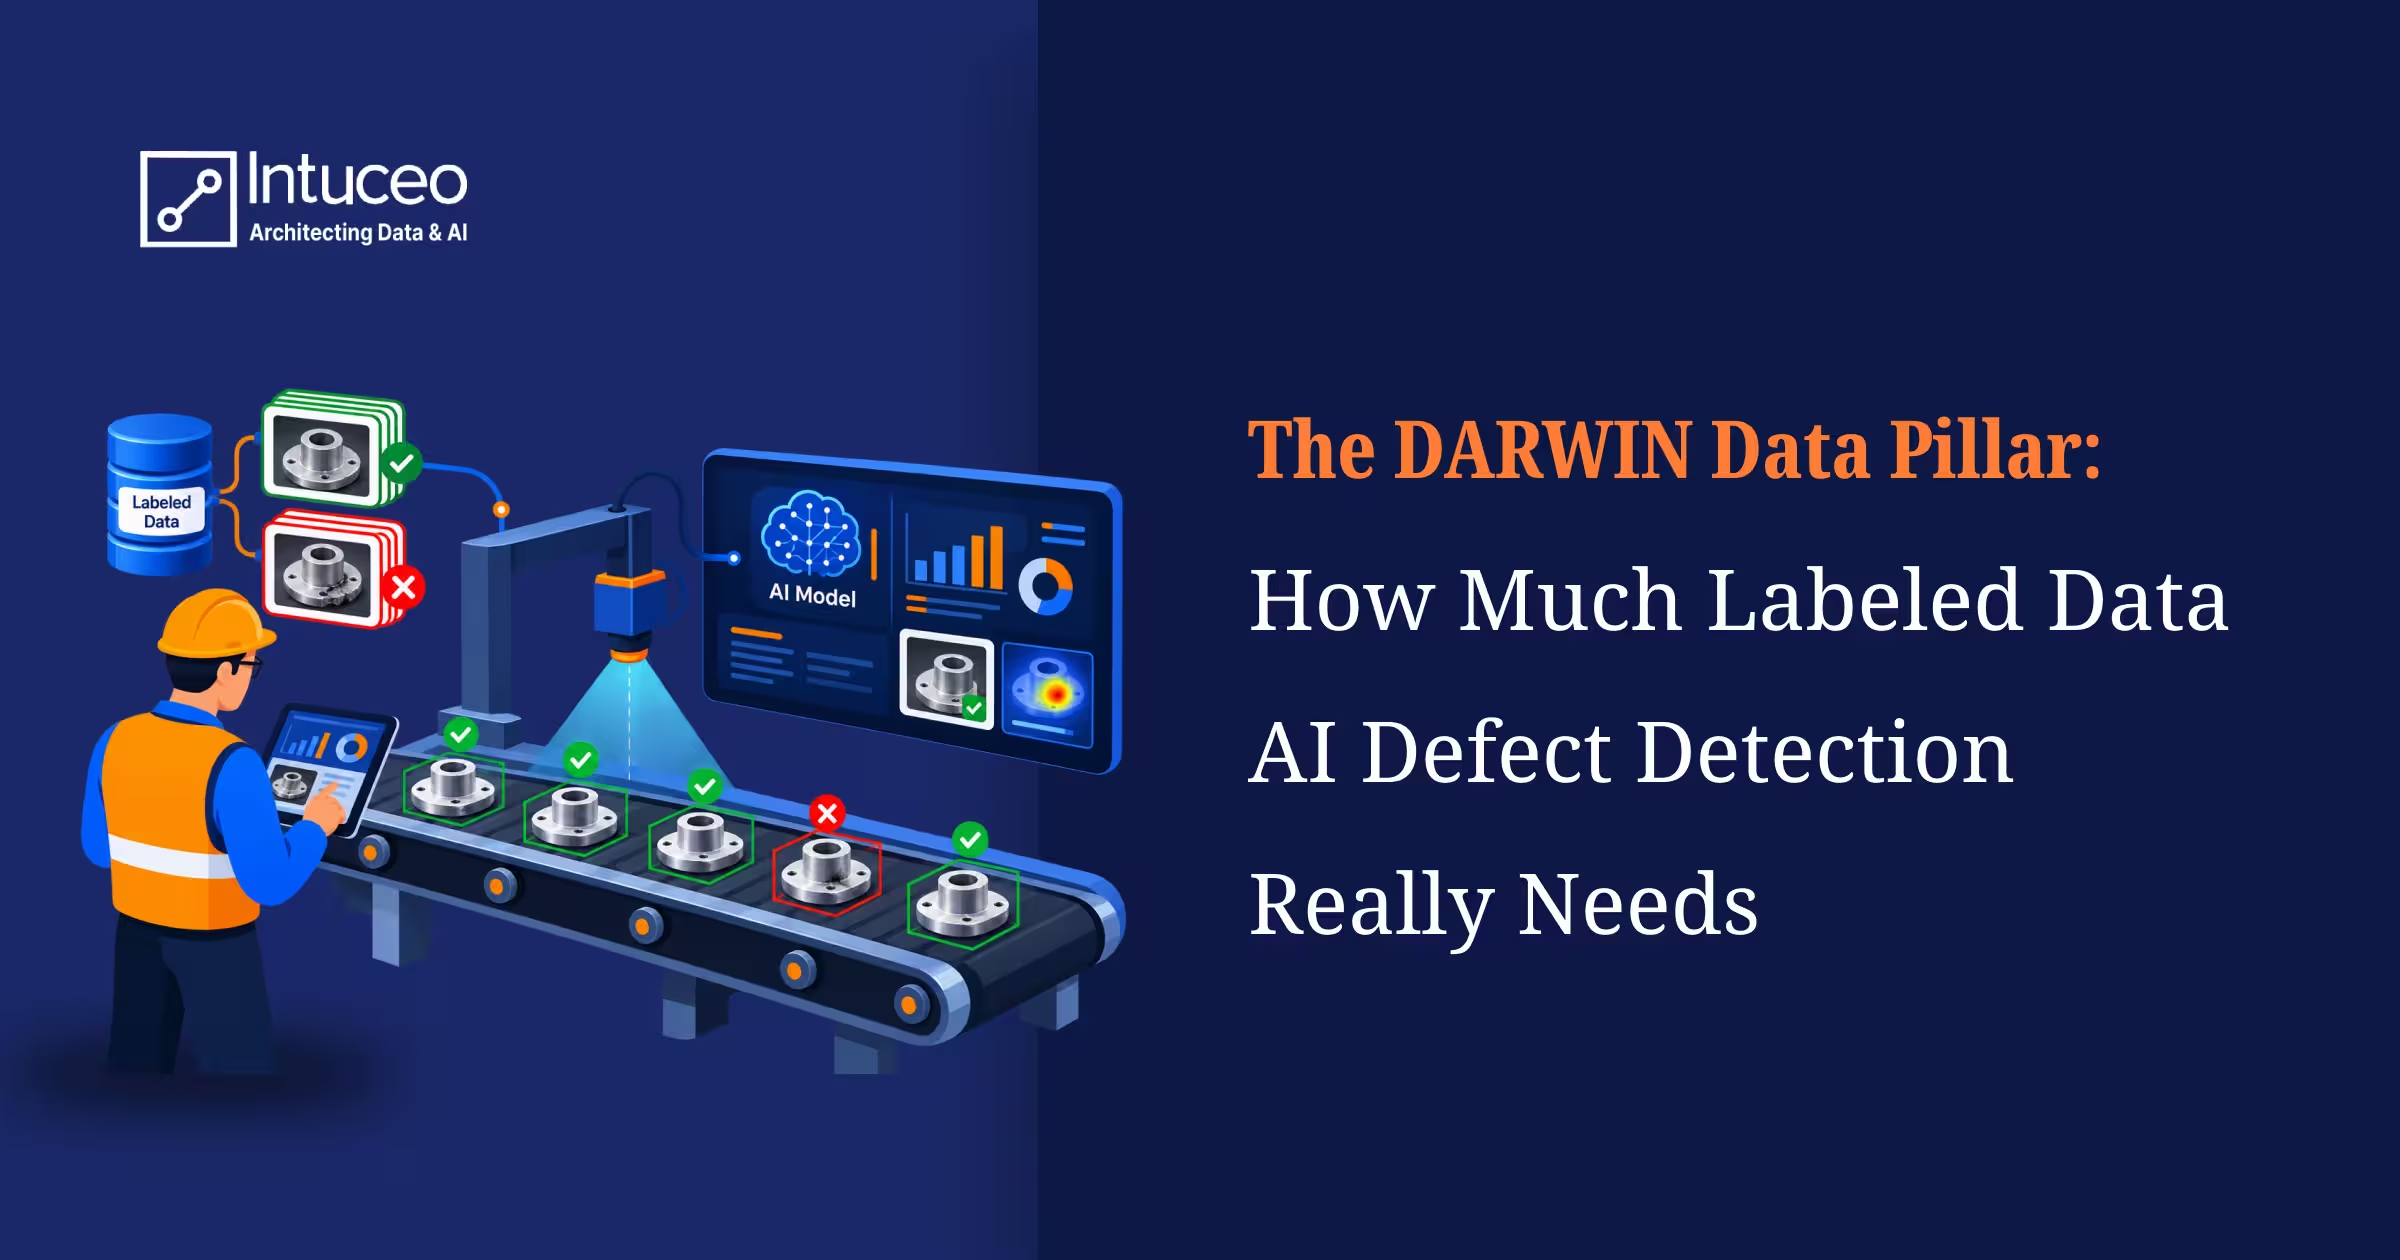
The DARWIN Data Pillar: How Much Labeled Data AI Defect Detection Really Needs

For years, the first question in any vision project was how many labeled images it would take. The answer was usually uncomfortable: thousands per defect class, drawn by people whose time was already committed elsewhere. That single estimate stalled many computer vision inspection projects before they began.
Newer models reduce how much labeled data AI defect detection needs in certain use cases, while other use cases still require the full effort. The Data pillar of the DARWIN™ Framework exists to separate the two before a budget is set.
This article explains how pillar sizes labeled data for AI defect detection within the DARWIN AI framework and what it means for manufacturing teams.

Key Takeaways

What Is the DARWIN™ Framework?

The DARWIN™ Framework is Intuceo AI Labs’ method for judging whether an AI initiative is ready for production across five dimensions: data, architecture, responsibility, workflow, and infrastructure and security. Intuceo AI Labs introduced it to help enterprises evaluate AI initiatives before committing to a build, asking whether each dimension is ready. The goal is a decision that can hold up after the pilot.
AI Dream Session, Vol. 1 set out the strategic question: what does an AI initiative need to move from idea to production? Vol. 2 applies that thinking to computer vision, where data questions tend to dominate.

What Does the DARWIN Data Pillar Ask Before Any Labeling Starts?

The Data pillar reframes the labeled data conversation around four questions.
Answering these before choosing a model prevents a common failure: collecting and labeling a large dataset for a problem that did not need one, or under-investing in a problem that did.

How Much Labeled Data Does AI Defect Detection Need?

Labeled data needs for AI defect detection depend on the decision the model supports. Presence checks and obvious anomalies may need only a small labeled evaluation set. Rare or surface defects can often start from images of good parts. Fine, low-contrast defects with tight tolerances still need substantial labeled examples per defect class.
There is no universal number, and anyone quoting one without seeing images is guessing. Published vendor guidance ranges from a few dozen to several hundred labeled images per defect class, a spread that reflects how differently use cases behave. What has changed is the range of workable starting points.
Broadly, manufacturing vision use cases now fall into three data profiles.
Data profile Typical use cases Labeled data needed
Zero-shot or prompted Part presence, region isolation, counting, obvious anomalies Small evaluation set only, to confirm performance
Few-shot or normal-only Rare defects, new variants, surface anomalies Images of good parts plus a modest labeled evaluation set
Fully supervised Fine, low-contrast defects with tight tolerances and strict acceptance criteria Substantial labeled examples per defect class
The middle row is where much of the change has happened. Research on anomaly detection shows how far performance can go with very little labeled data. WinCLIP, a method built on a vision-language model, reports 91.8% area under the receiver operating characteristic curve (AUROC) for zero-shot anomaly classification on the MVTec AD industrial benchmark, rising to 93.1% for its variant using a single normal image[1].
Treat that as proof of direction, not a promise. On VisA, a second industrial benchmark, the same method scores 78.1% AUROC zero-shot, a reminder that results move with the data[1]. Benchmark images are cleaner and more consistent than most plants. Your results depend on your parts, defects, and imaging conditions.

Why Labeled Data for AI Defect Detection Shrinks but Never Disappears

Labeled data reduction is real. Elimination is not. Even the most data-efficient approach needs labels in three places:
The shift is in proportion. Instead of labeling thousands of training images upfront, teams increasingly treat labeled data for AI defect detection as a smaller, sharper set that proves performance and tracks it over time.

Which Data-Efficient AI Models Reduce Labeling for Defect Detection?

Data-efficient AI models reduce labeling in several ways, each suited to different situations:
Choosing among them is a Data pillar decision because it depends on what data exists, how rare the defects are and how precise the decision must be.

What Makes Training Data for AI Defect Detection Reliable?

When training data for AI defect detection is needed, quality consistently matters more than volume, a pattern we see across AI deployments in advanced manufacturing. A few practical principles apply:

Why Does Data Governance Matter More for Lean Vision Datasets?

Smaller datasets carry less redundancy, so data governance for vision AI matters more, not less. Governance for vision work covers who owns image data, how labels are reviewed and approved, how long images are retained, and how changes on the line trigger revalidation. In regulated environments such as life sciences manufacturing, it also covers traceability and audit readiness.
One caution: a reduced labeling plan without a drift monitoring plan simply moves the risk from build time to run time.

How Do You Know If Your Labeling Plan Is Too Big or Too Small?

The Data pillar also helps teams spot a mismatch between effort and need, and shows where it is safe to reduce labeled data for defect detection. Watch for these signals.

Likely oversized

Likely undersized

Undersized plans tend to show up as disappointing pilots. Oversized plans show up as projects that never start. Both are expensive, which is why the Data pillar treats labeling as a decision to justify rather than a default.

How to Build a Labeled Data Plan for Manufacturing Vision AI in Six Steps

A practical plan for labeled data requirements in manufacturing vision AI starts small and grows with evidence:
1. Inventory archived images, reject records, and existing defect definitions.
2. Match each use case to a data profile: zero-shot, few-shot, or fully supervised.
3. Build a labeled evaluation set first, before any training data.
4. Test the lightest viable approach against that set.
5. Add labeling effort only where results fall short of acceptance criteria.
6. Put monitoring and governance in place before production, not after.
Want a second view on your labeling plan? Scope your vision use case with an AI architect.

How Intuceo supports the data work

Intuceo’s DataOps and engineering team prepares, versions and governs the data that vision models depend on, while Intuceo AI Labs applies the DARWIN™ Framework to decide how much of it a use case genuinely requires. In Intuceo’s lens defect detection work for precision optics, the vision model reduced manual QA workload by up to 30%.

Watch: Computer Vision Reimagined, On Demand

AI Dream Session, Vol. 2: Computer Vision Reimagined is a 45-minute session with Intuceo AI Labs on how newer vision models reduce dependence on large labeled datasets, and where they do not. It is now available on demand.

Frequently Asked Questions

The DARWIN™ Framework is Intuceo AI Labs’ method for judging whether an AI initiative is ready for production across five dimensions: data, architecture, responsibility, workflow, and infrastructure and security. It was introduced in AI Dream Session, Vol. 1, and Vol. 2 applies it to computer vision.
It matches each use case to the lightest viable data approach before any labeling begins, then adds effort only where testing against acceptance criteria shows it is needed, rather than committing to a large training set by default.
There is no reliable universal minimum of labeled data for AI defect detection. The one constant is a labeled evaluation set from your own line to validate performance; beyond that, requirements scale with how fine and tightly toleranced the defects are.
Validate against a labeled evaluation set first, then reach for the data-efficient approaches above before committing to full supervision. Keep the hardest examples in the set and monitor for drift so the leaner dataset stays trustworthy.
Often, yes, for rare or surface defects. Normal-only anomaly detection learns from good parts and flags departures. You still need a small labeled evaluation set from your own line to confirm it meets acceptance criteria.
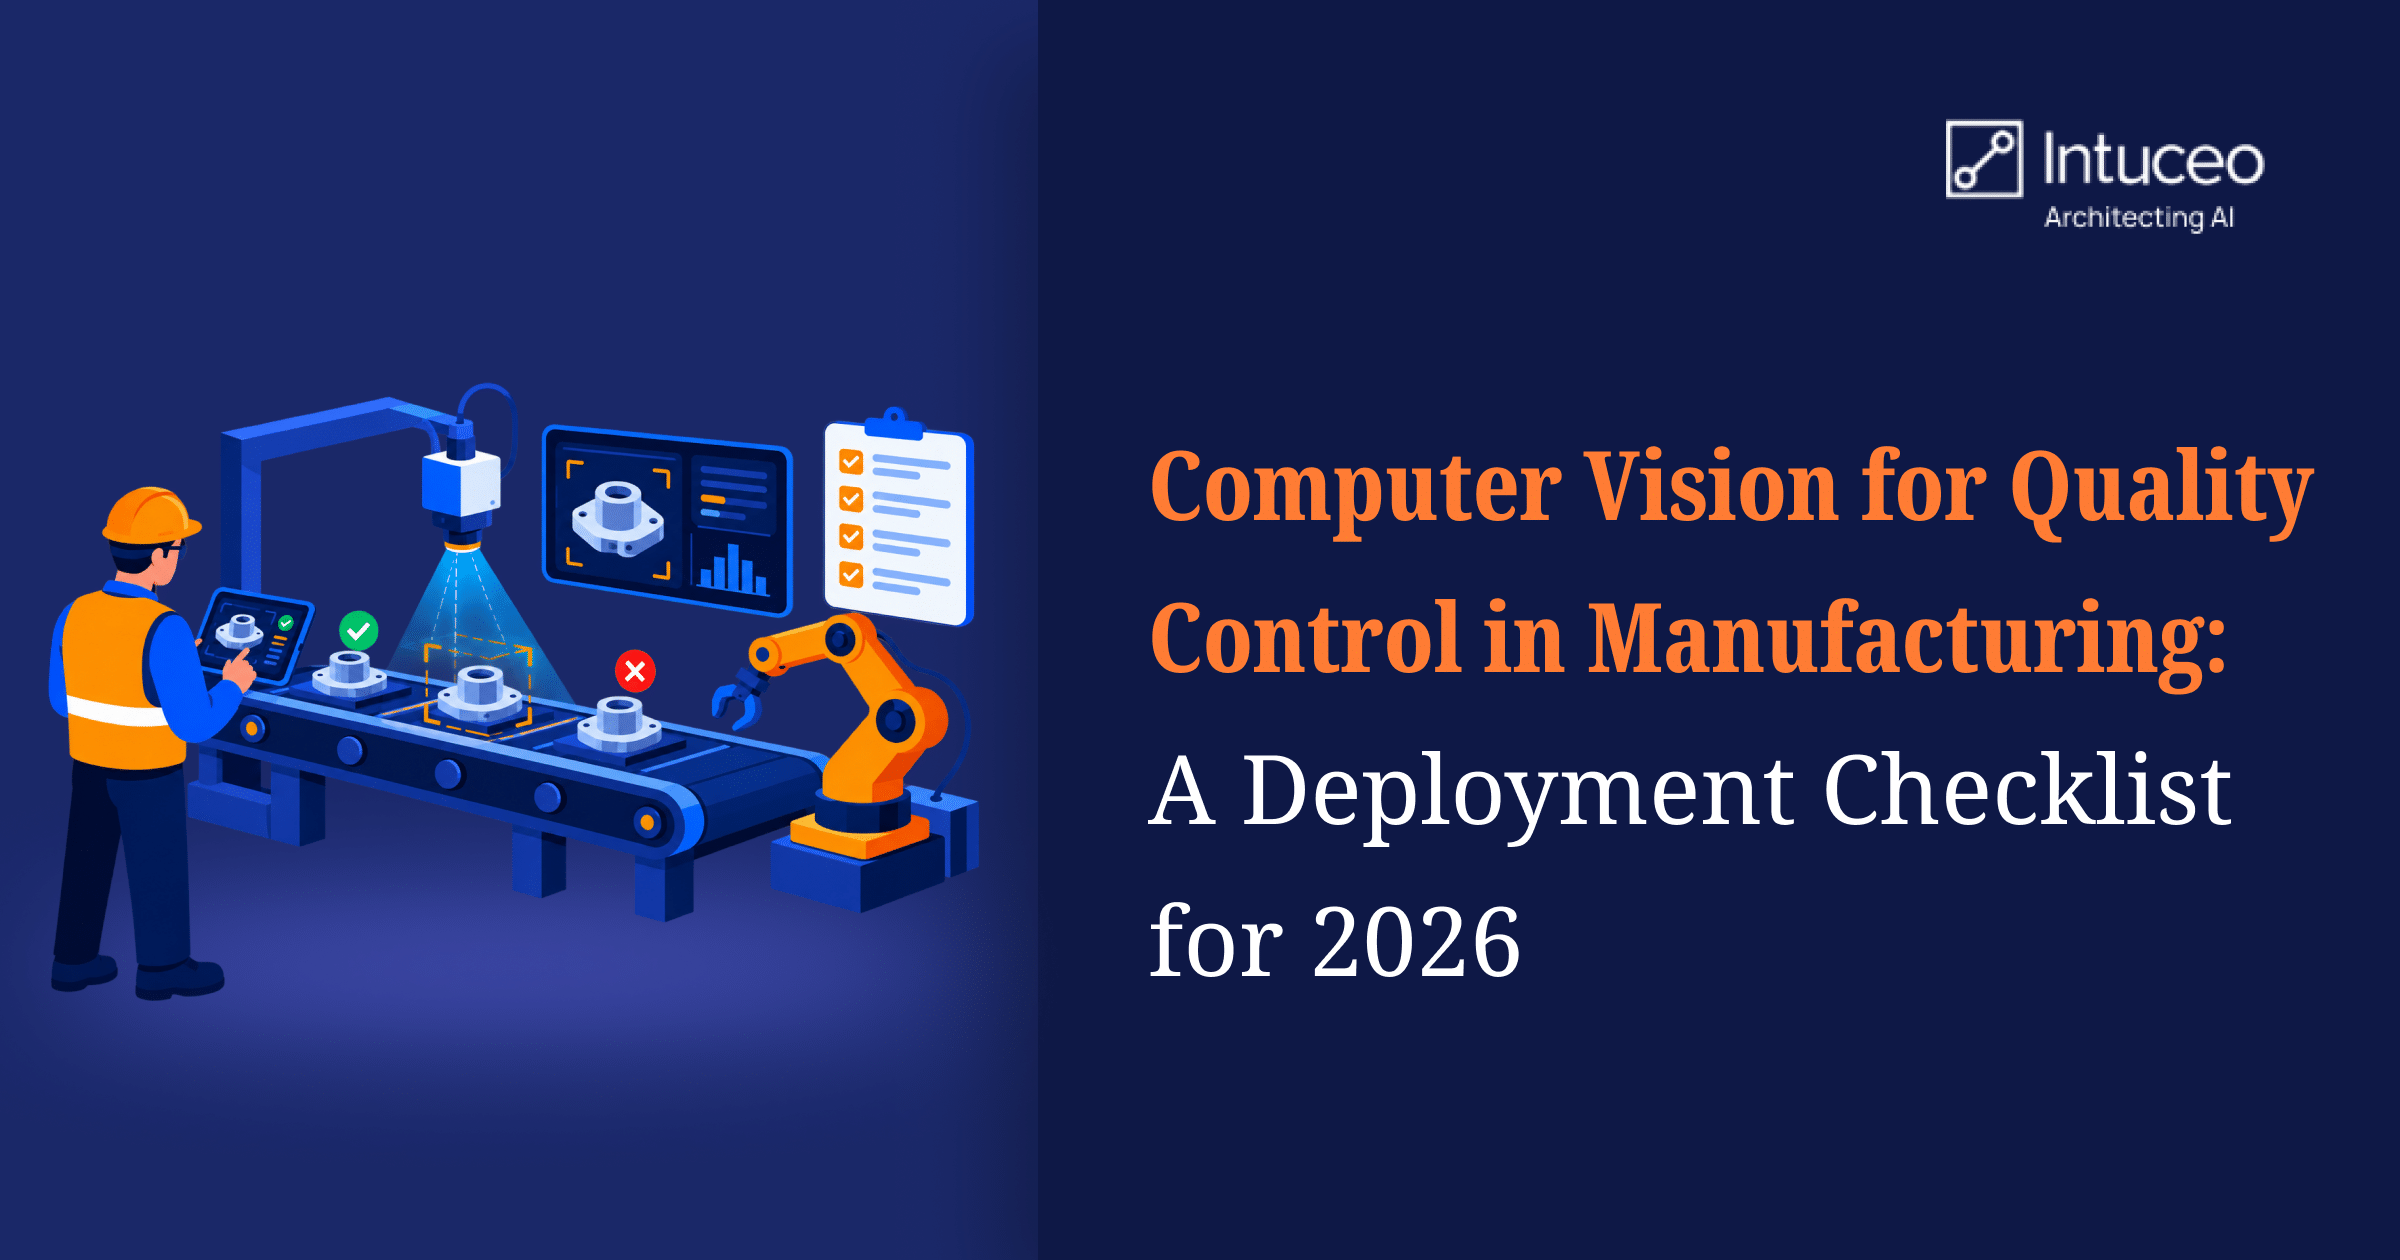
Computer Vision for Quality Control in Manufacturing: A Deployment Checklist for 2026

Quality escapes rarely announce themselves on the inspection line. They surface later as returns, warranty claims, containment actions, and a customer relationship that cools a degree at a time. For manufacturers running high-mix lines across Florida’s aerospace, defense, medical device, electronics, and marine sectors, catching defects earlier has moved computer vision quality control from pilot curiosity to a line-of-business decision.
The state gives the question real weight. Florida employed roughly 430,000 people in manufacturing as of mid-2026, [1] much of it in small and mid-sized plants where a poorly run rollout is a costly detour. For those operations, the discipline of the deployment matters more than the brand of camera on the bracket.
What follows is a working computer vision quality control checklist. A buyer can use it to run a deployment and to judge a vendor’s rigor; a vendor can treat it as a delivery standard.

Key Takeaways

What Is Computer Vision Quality Control, and What Does It Change?

Computer vision quality control is the use of cameras, controlled lighting, and trained Artificial Intelligence (AI) models to inspect every part on a line and trigger a pass, reject, or alert in real time. An AI visual inspection system does not replace a quality program; it changes where and how consistently the program catches problems. A camera captures each part, a trained model scores it against the definition of a good unit, and the line acts on that score in real time rather than at a sampling gate hours later.
The value is consistency. Trained human inspectors are estimated to miss defects in 20 to 30 percent of cases, with performance varying by experience, fatigue, and how often a given defect actually appears. [2]
Automated visual inspection holds one standard across every part and every shift, and it produces a record of each decision that a manual gate cannot.
Two capabilities carry most of the load on the floor.
Defect detection AI trained on labeled examples handles the faults you can describe and show, while anomaly-based models flag parts that simply deviate from normal, including defect types no one has catalogued yet. Together they give machine vision quality assurance a reach that rule-based optical inspection, manually tuned for each condition, struggles to match. Classical Automated Optical Inspection (AOI) still fits stable, well-lit, unchanging parts, but it needs manual reprogramming whenever a part or a defect shifts, which is precisely where trained models earn their place on mixed lines.
The table below compares the three approaches on a production line.
Dimension Retrospective approach AI-led approach
Timing Year-end chart chase Year-round, starting early in the measurement year
Prioritization All open gaps treated alike Gaps ranked by how likely they are to close
Data used Claims and a sample of charts Claims, clinical notes, lab results, and health information exchange feeds
Outreach Generic reminders Member-specific, in the member’s language
Audit readiness Manual reconstruction Lineage from source to measure

How to Deploy Computer Vision Quality Control: A Six-Step Checklist

Most stalled computer vision quality control deployments fail on fundamentals set in the first two weeks, not on model choice. Work the sequence in order.

Step 1: Define the Defect and the Cost of Missing It

Write down what pass and fail mean in physical terms, and attach a cost to each escape. A scratch that fails a medical housing and a scratch that fails a boat fitting are not the same decision, and the model is only as clear as that definition.

Step 2 : Fix the Imaging Before the Model

Resolution, lens, working distance, and above all lighting decide whether a defect is visible to the sensor at all. Controlled lighting and consistent part presentation remove more error than any later algorithm tuning, so settle the optics and fixturing first.

Step 3 : Build a Labeled Dataset That Reflects the Line

Collect images of good and defective parts across the real range of shifts, materials, and lighting, and label them with the people who own the quality standard. Rare defects are the hardest to gather and the most expensive to miss, so plan deliberate collection rather than waiting for them to appear.

Step 4 : Choose the Model Approach and Where It Runs

Match the method to the problem, using supervised detection for known, describable defects and anomaly detection where faults are rare or ill-defined, and score parts at the line for speed and data control. On-line scoring keeps pace with production and keeps sensitive part data inside the plant.

Step 5 : Integrate With the Line and Business Systems

A pass or fail signal is only useful if it drives an action, whether a reject arm, an operator alert, or a logged record. Wiring results into the Manufacturing Execution System (MES) and the Enterprise Resource Planning (ERP) system turns inspection into traceable quality data and ties a defect back to the batch, machine, and shift that produced it.

Step 6 : Validate, Monitor, and Plan to Retrain

Prove the system against known samples before it gates real production, then watch for drift as parts, materials, and cameras change over time. A model that was accurate at go-live decays quietly without monitoring and periodic retraining.
On the high-mix, lower-volume lines common in Florida aerospace and medical device work, steps three and six carry the most weight, since every new part variant reopens the dataset and validation questions.

How to Calculate Computer Vision ROI in Manufacturing

The computer vision ROI (Return on Investment) in a manufacturing setting comes from a few specific places, and it helps to name them rather than quote a single payback figure.
The largest is usually the cost of escapes avoided : the returns, warranty exposure, and containment events a missed defect sets in motion downstream. Earlier detection reduces scrap and rework, because a fault caught at the station that created it wastes far less material and labor than one caught at final assembly. In most rollouts, the first recovered cost is the drop in escaped defects on the highest-value parts, followed by scrap savings once detection moves upstream to the station of origin.
Two further effects show up over time. Inspectors move from repetitive scanning to handling the genuinely ambiguous cases the model flags, a better use of scarce skilled labor. And the decision record the system produces becomes an audit trail that carries real weight in regulated Florida sectors such as medical devices and aerospace.
ROI tracks the cost of your defects and your production volume, so the honest first move is to model your own numbers against the checklist above before committing to a line-wide rollout.
Price the deployment over its life rather than at go-live alone, since labeling, revalidation, and periodic retraining are recurring costs a fair proposal names up front. That same modeling answers the tool question: the right system for defect detection in 2026 is the one that fits your defect, your throughput, and your integration reality, not the one with the longest feature list.

What Should Florida Manufacturers Look for in a Computer Vision Partner?

The most challenging aspects of a deployment are imaging, labeled data, and the integration into systems that were never meant to receive a vision signal.
This is where a services partner earns its place, and where evaluation criteria matter more than a spec sheet: relevant defect and sector experience, a clear labeling and validation method, and the ability to connect inspection to MES and ERP rather than leaving a camera stranded on the line.
Intuceo, a Jacksonville-based AI and data engineering services firm, helps businesses with computer vision as one capability inside a broader manufacturing and data practice. Its work applies machine learning to MES and sensor data to identify process variances and defect signatures before parts are produced, which places inspection inside the wider quality picture rather than only at the end of it. In Intuceo’s lens defect detection work, high-speed vision models reduced manual QA workload by up to 30 percent while increasing inspection accuracy.[3] Those systems run on Intuceo-Dx, its pre-built computer vision and document intelligence accelerator within the Modular AI suite.
For Florida manufacturers weighing a first computer vision quality control deployment or a wider rollout, the practical next step is a scoped assessment of one line against the checklist above.

Scope your first inspection line, not a year-long program

Map one line to a deployment plan: defect definition, imaging, data, integration, and a defensible ROI case, before you commit capital across the floor.

Frequently Asked Questions

The ROI of computer vision quality control comes mainly from escapes avoided, meaning the returns, warranty exposure, and containment costs a missed defect triggers downstream, plus reduced scrap and rework from catching faults at the station that caused them, and a better use of skilled inspectors. No single payback figure transfers across plants, so the sound approach is to model one line against your own defect costs and volume before scaling.
Deploy a computer vision inspection system in six steps: define pass and fail in physical terms, fix the imaging and lighting, build a labeled dataset that reflects your real production range, choose a model approach suited to your defects, integrate results into the line and your MES and ERP systems, then validate against known samples and monitor for drift. The imaging and data steps decide most outcomes, so resist starting with the model.
The best sensor is the one that makes your specific defect visible, which is a function of defect size, surface, and line speed rather than raw megapixels. Area-scan cameras suit discrete parts, line-scan suits continuous or cylindrical material, and 3D or specialized sensors handle depth, gloss, or sub-surface issues. Lighting and lens choice usually matter more than the camera body.
Computer vision integrates with MES and ERP systems by passing each inspection result as structured data to the Manufacturing Execution System, which links each pass or fail to the batch, machine, and shift, and onward to the ERP system for quality, traceability, and cost reporting. Integration usually runs through the MES layer or an intermediate connector, and it is what converts a camera’s verdict into quality data the business can act on.
It is more consistent. Trained inspectors are estimated to miss 20 to 30 percent of defects depending on experience and fatigue, while an automated system applies one standard to every part and every shift and logs each decision. Accuracy still depends on imaging, labeled data, and ongoing monitoring.

Supply Chain AI in Florida: How Ports, Logistics Hubs, and Transportation Leaders Are Cutting Lead Times

The 2026-2030 Florida Seaport Mission Plan, published by the Florida Seaport Transportation and Economic Development Council, directs investment toward dock rehabilitation, capacity expansion, cargo container handling and connectivity across the state’s publicly owned seaports. Physical throughput is being funded. The sequencing logic above it is not being funded at the same pace, and that is where most delay now accumulates.
For anyone evaluating supply chain AI in Florida, the starting point is this: lead time in a freight network rarely disappears at one point. It leaks across handoffs: vessel to yard, yard to gate, gate to drayage, drayage to distribution center, distribution center to customer.
Each handoff carries its own system of record, reporting cadence, and definition of an exception. By the time a planner identifies the problem, the cost is booked. That gap is what Florida operators are now adopting AI to close.

Key Takeaways

Where does lead time leak in Florida freight networks, and how do you measure it?

The Bureau of Transportation Statistics runs the Port Performance Freight Statistics Program, which publishes nationally consistent measures of capacity and throughput for United States seaports, including containership and tanker berthing times updated weekly. [2] It gives operators an external reference point for berth performance.
To measure lead-time leakage before modeling, timestamp each handoff, calculate the median and 90th percentile wait at each one, and rank handoffs by the cost of delay.
Mechanization raises the ceiling. PortMiami has been expanding the fleet of electric rubber-tired gantry cranes at its South Florida Container Terminal, allowing higher container stacking and shorter runs within the yard.
More cranes increase how many moves are possible in an hour. Whether those moves happen in the right order, against the right truck appointments, is a different question that AI for Florida ports is positioned to answer.
Dwell time, the time a container sits in the terminal between discharge and pickup, falls when three things line up: the yard knows which container is wanted next, the gate knows which truck is arriving to collect it, and the carrier knows before arrival whether the slot still holds. Each of those is an AI prediction problem sitting on data that already exists in terminal operating systems, electronic data interchange feeds, and telematics streams.

How does Florida's 2026 data center law (SB 484) affect supply chain AI?

Florida enacted CS/CS/SB 484 as Chapter 2026-65, with most provisions effective July 1, 2026. [4] The law requires the Public Service Commission to implement tariff and service requirements ensuring that large load customers such as large data centers pay their own cost of service, with the risk of nonpayment kept off the general body of ratepayers.
Utilities were required to file conforming tariffs for approval by October 1, 2026. The law also bars any tariff, contract, or utility policy from preventing or hindering curtailment of service to a large load customer when it is necessary to maintain grid stability or protect public safety during emergencies, and prohibits service to large load facilities owned or controlled by foreign countries of concern. [5]
Two consequences follow for anyone deploying Florida logistics AI.
Provision What it means for AI buyers
Large load customers, such as large data centers, must pay their own cost of service. Inference becomes a priced, visible operating line rather than an assumption. Designs that call a large model for every event will carry a different cost profile in Florida than they did in a vendor demonstration.
Tariffs and contracts cannot prevent curtailment of service to large loads during grid emergencies. Compute hosted in-state is explicitly interruptible during grid emergencies. Grid emergencies in Florida cluster in storm season, precisely when routing, diversion and inventory decisions carry the most value.
A decision layer that stops working when the weather turns is worse than no decision layer, because operators will have stopped maintaining the manual process it replaced.
Design implication: keep the models that must survive a disruption small, local and deterministic in their fallback. Reserve heavier reasoning for planning cycles that can tolerate a pause.

Does Florida regulate AI? Why procurement contracts carry the governance load

The proposed Artificial Intelligence Bill of Rights was designed to impose conditions on government contracts for AI technology. It cleared the Senate in March 2026 and then died in the House. [6] A second attempt during the April special session cleared the Senate again and died in House subcommittee the following day. [7]
Florida’s port authorities are governmental entities, which puts their AI vendors in the same position as other Florida government contractors. In the absence of a statutory standard, the obligations a buyer wants have to be written into the contract, not inherited from the code.
For Florida buyers of transportation analytics, four contract terms are worth insisting on:
Vendors should read the same signal in reverse. An offering built around accuracy claims alone is harder to defend to a Florida public sector buyer than one built around evidence. Reshaping a service line to lead with explainability, integration commitments, and exit terms is now a commercial advantage rather than a compliance overhead.

Where should supply chain AI in Florida start? Four decisions to automate first

Most Florida operators do not need a network-wide program. They need to get four decisions right :

Demand and inventory positioning

Forecasting that harmonizes historical movement with live market signals changes where stock sits before the order arrives. This is the core of Florida distribution center analytics: fewer emergency freight bookings, less inventory held against uncertainty, and replenishment triggered by a signal rather than a calendar.

Procurement and dispatch

Carrier selection, share-of-business allocation and container utilization are optimization problems with clear constraints. Routing intelligence that removes empty running takes cost out without touching headcount or assets.

Multi-modal visibility

Rail, road and sea data arrive in different formats on different clocks. A single reconciled record per shipment is the prerequisite for everything else, and it is usually the hardest part of the build.

Freight audit and billing reconciliation

Invoice and proof-of-delivery matching recovers money that is already owed. It is the fastest route to a defensible return, and it builds the internal credibility needed for the larger work.
Intuceo, a Jacksonville-based enterprise AI consultancy, built its iTMS supply chain accelerator to address these four as connected modules, with supervisory agents monitoring forecasting, planning, and execution.
Across deployments, Intuceo reports a 30% increase in forecasting accuracy and billing reconciliation accelerated by 40%. The accelerator is deployed as a layer over existing enterprise resource planning and electronic data interchange estates rather than a replacement for them, which matters in Florida, where mainframe and legacy carrier integrations remain in daily service.

Why Jacksonville matters for port, rail, and logistics AI

Northeast Florida is where sea, rail and highway freight converge most tightly. The Jacksonville Port Authority (JAXPORT) runs its cargo terminals in the same city as Class I rail headquarters, which puts the handoff between sea and rail inside one metropolitan area.
Conversations about logistics AI in Jacksonville therefore tend to start at the interchange rather than at the berth, because a container that clears the terminal quickly and then waits on a rail slot has not saved anyone a day. Intuceo is headquartered in Jacksonville and has delivered supply chain and transportation work for operators including CSX and the MTA Long Island Rail Road (LIRR). Proximity matters: the data that makes these models work is held by yard supervisors, dispatchers, and billing clerks, and it can be extracted much faster in person than over a call.

How to choose a supply chain AI consulting partner in Florida

Put a number on where your lead time goes

Intuceo’s supply chain diagnostic baselines one lead-time metric in your Florida network, identifies where it leaks across handoffs, and returns a costed plan to close it within 90 days.

Frequently Asked Questions

The applications with the clearest effect are berth and yard sequencing, gate appointment matching, and predicted container availability shared with drayage carriers before they arrive. Each one shortens the interval between a container becoming available and a truck collecting it. Capital investment in yard equipment raises the number of moves that are physically possible; sequencing intelligence determines how many of them are the right moves.
Supply chain AI in Florida is typically bought in one of three forms: modules inside an incumbent transportation management system, standalone visibility services, or accelerator-led engagements from services firms that build on top of existing systems. The third suits operators with substantial legacy integration, since it avoids a migration. Intuceo’s iTMS accelerator sits in that category, covering forecasting, dispatch, multi-modal visibility and freight audit as connected modules.
AI helps Florida distribution centers manage inventory in real time by replacing periodic stock reviews with continuous signals. Demand models informed by inbound vessel schedules, order patterns and carrier performance indicate what should be positioned where, and how much buffer is genuinely required. The practical result is fewer expedited shipments and less capital held against uncertainty, with exceptions surfaced while they can still be acted on.
There is no single best platform; the best fit depends on the systems you already operate. Buyers running modern cloud systems can often extend them. Buyers running mainframe, legacy electronic data interchange or long-standing carrier integrations, which describes much of Florida’s rail and port ecosystem, generally get further with a services-led engagement that layers intelligence over those systems. Evaluate AI consulting partners in Florida on integration record, explainability, time to a measurable result, and their willingness to commit to a defined first metric.
Not as of this writing. Florida has no general AI statute. The proposed Artificial Intelligence Bill of Rights, which would have set conditions on government AI contracts, passed the Senate twice in 2026 but died in the House both times. Buyers, including port authorities, have to write explainability, data residency, and audit requirements into contracts.
Intuceo scopes its supply chain diagnostic to deliver a baseline and costed plan within 90 days, and iTMS deployments typically reach a live pilot with measurable ROI in about 90 days.

Zero-Shot Segmentation in Manufacturing: What It Can and Cannot Do

Segmentation has long been one of the most labor-intensive steps in a vision project. Every defect, component edge, or region of interest had to be outlined by hand, pixel by pixel, often across thousands of images.
Promptable foundation models changed that cost structure, at least in principle. An object can now be pointed at, or described, and a mask returned without task-specific training.
The question for quality and engineering teams is how much of that holds up on a real line. While zero-shot segmentation in manufacturing is useful for a defined set of jobs, it is unsuitable for others. This guide separates the two, explains why, and sets out a practical way to test it before anyone commits budget.

Key Takeaways

What zero-shot segmentation means in industrial inspection

Segmentation assigns each pixel in an image to a region: this area is the part, that area is a scratch, the rest is background. Traditional segmentation models learn those regions from hand-drawn masks on the exact task they will perform.
Zero-shot segmentation skips that task-specific training. A foundation model pretrained on a very large, general dataset is prompted at runtime with a point, a bounding box, or, in some setups, a text description, and returns a mask. The best-known example is Meta AI Research’s Segment Anything Model (SAM). Its authors assembled a dataset of over 1 billion masks on 11 million licensed images and trained the model to be promptable so that it transfers zero-shot to new image distributions and tasks.
That scale is the reason the approach generalizes. It is also the reason for caution. None of those images were taken on your line, under your lighting, of your product parts.

Where zero-shot segmentation performs well

The strongest fits share one trait: the region being segmented is visually distinct from its surroundings.
In each case, the model performs localization. It reports where something is. A separate step decides whether that something is acceptable.

Where zero-shot segmentation is unreliable

The limitations map closely onto the defect types manufacturers care about most.

Fine and low-contrast defects

Hairline cracks, micro-scratches, faint discoloration, and subtle porosity often lack clear edges. The SAM authors state that the model can miss fine structures, sometimes generates small disconnected components, and does not produce boundaries as crisply as more computationally intensive methods.[1] On a production line, a missed hairline crack is not a small error to be overlooked.

Acceptance criteria

A mask is not a verdict. The model can outline a mark on a surface without any sense of whether that mark is cosmetic, within tolerance, or cause for rejection. Acceptance criteria live in your quality system, not in a general-purpose model.

Consistency across imaging conditions

Glare, reflective metal, transparent packaging, and shifting ambient light can change results from one frame to the next. The absence of task-specific training does not reduce a model’s sensitivity to imaging conditions.

Speed at line rate

Large foundation models are computationally heavy. Where a decision must be made inside a single machine cycle, the full model may not keep pace without dedicated hardware or a lighter distilled version.

Zero-shot detection vs. segmentation: which does your inspection need?

The two terms are often blended, and the difference affects system design. Zero-shot detection in industrial inspection draws a box around a candidate and assigns a label. Zero-shot segmentation draws the outline. Detection is usually sufficient for presence, position, and counting, and it costs less to run. Segmentation earns its additional compute when shape, area, or boundary precision matters, such as measuring a coating gap or the extent of a surface defect.
Aspect Zero-shot detection Zero-shot segmentation
Output A box and a label A pixel-level outline (mask)
Best for Presence, position, and counting Shape, area, and boundary precision
Compute cost Lower Higher
Example Confirming a part is present Measuring a coating gap or defect extent
Teams often chain the two. An open-vocabulary detection model locates candidate regions from a text prompt in production, and a segmentation model outlines what sits inside each box.

Where does the Segment Anything Model (SAM) fit in manufacturing workflows?

The roles above differ mainly in how much human judgment sits between the mask and the decision, and that is what should order a SAM manufacturing rollout. Exploratory analysis of archived images carries no line risk, because nothing reaches production. Annotation assistance comes next, because an engineer approves every mask before it becomes training data. Preprocessing follows, since a trained classifier still makes the call on the cropped region.
A fourth role, treating the model as the final accept-or-reject authority, is where most disappointment occurs. It is rarely the right starting point.

How do vision-language models and segmentation models work together?

Foundation models for visual inspection increasingly work as a set rather than alone. A vision-language model can be asked whether an image shows anything unusual and to describe it. A segmentation model then outlines the region it points to. That pattern is behind most current interest in vision-language models for defect detection, particularly for unfamiliar anomalies. It also stacks two sources of uncertainty, so validation on your own images matters more.

How do you test zero-shot segmentation on your production line? 7 steps

A short, structured test answers most questions before a full project starts. Seven steps cover the ground.
  1. Assemble a hard evaluation set: Include your subtle defects, reflective parts, and worst lighting, not only clear examples.
  2. Define success in operational terms: Mask overlap scores are useful, but the decisive question is whether the mask would lead to the right part disposition: accept, rework, or reject.
  3. Compare prompt types: Points, boxes, and text prompts behave differently. Test the one you would actually use in production.
  4. Measure speed on target hardware: Benchmark on the device that would sit near the line, not a research workstation.
  5. Repeat across shifts and variants: Run the same prompts on images from different shifts, operators, lighting states, and a recent part variant, to see whether performance holds without adjustment.
  6. Record how it fails, not only how often: A model that misses in predictable ways is easier to manage than one that fails at random, and a clear list of what it misses is as valuable as an accuracy score.
  7. Check review time and traceability: If reviewing uncertain masks takes longer than manual inspection, the workflow needs redesign. Record model version, prompt, and image for each output so decisions can be audited later, a standard practice in production MLOps pipelines.
If a zero-shot model performs well only after heavy prompt tuning on a handful of images, run the same prompts on a fresh batch before trusting the result. Overfitting prompts is easier than it looks.

When should you move from zero-shot to a fine-tuned model?

Move beyond zero-shot when fine defects dominate, tolerances are tight, or decisions must be made within a machine cycle. Zero-shot segmentation for industrial inspection is often the fastest way to learn whether a computer vision inspection project is tractable, but it is not always the final answer. In those cases, the usual next step is fine-tuning on a modest set of your own images or distilling results into a smaller model.

How Intuceo approaches segmentation work

Intuceo starts with the inspection decision the business needs, then works backward to whether segmentation, detection, or a simpler rule is the right tool. Scope your inspection use case with an AI architect.

Two capabilities carry most of the delivery on vision work. High-fidelity visual inspection applies image segmentation, sub-pixel anomaly detection, and automated feature extraction to sub-millimeter defects, including precision medical optics, where surface anomalies, edge irregularities, and contaminants have to be caught at production speed. Multi-modal vision intelligence brings video, image, and metadata streams together so inspection results arrive alongside line system signals rather than in a separate console.

Deployment is the part that has to survive audit. Intuceo delivers in on-premise, private cloud, and air-gapped environments, driven by PhD-led engineering teams with prior deployments in regulated and high-precision environments. See how this applies across AI-driven advanced manufacturing and to the ML and computer vision capability built for it.

Join AI Dream Session, Vol. 2: Computer Vision Reimagined

AI Dream Session, Vol. 2: Computer Vision Reimagined is a 45-minute live session with Intuceo on Thursday, September 24, 2026, at 11:00 AM ET. It covers how newer vision models reduce dependence on large labeled datasets, and where accuracy and production conditions still create hard problems.

Frequently Asked Questions

It is the ability to outline objects or regions in an image using a pretrained foundation model, guided by a prompt such as a point, box, or text description, without training on your specific parts. In inspection, it is most often used to isolate components, extract regions of interest, and speed up labeling, rather than to make final quality decisions on its own.
Not entirely. They can sharply reduce the labeling needed to get started and can pre-label images for engineers to correct. You still need a labeled evaluation set from your own line to confirm performance, and many subtle defect types still benefit from fine-tuning on examples specific to your process.
Four limits dominate: weak performance on fine or low-contrast defects, no built-in understanding of acceptance criteria, sensitivity to glare and lighting changes, and heavy compute requirements for large models.
Yes, in well-chosen roles: annotation assistance, preprocessing that isolates parts or regions, and exploration of archived images. Using them as the sole accept-or-reject authority is riskier.
Not always. Large foundation models are computationally heavy, so decisions inside a single machine cycle may need dedicated hardware or a smaller distilled model.

A Decision Framework for Revisiting Shelved Computer Vision Inspection Projects in Manufacturing (2026)

Many plants carry at least one computer vision inspection initiative that cleared a pilot and then went quiet. The reasons were usually sound. The defect was too rare to build a training set. Parts changed faster than the model could be retrained. The labeling bill outgrew the savings, or integration with the line took longer than anyone had budgeted.
Vision models have moved on since then, and some of the constraints that stopped a computer vision inspection program in manufacturing have loosened-while others have not. For operations and quality leaders, the task is sorting shelved computer vision projects into three groups: the ones newer AI makes worth a revisit, the ones that need a scoped test first, and the ones that should stay exactly where they are. This framework is built for that sort.
KEY TAKEAWAYS

Why Computer Vision Inspection Projects in Manufacturing Get Shelved

Before scoring anything, name the real reason each project stopped. Most paused AI projects in manufacturing trace back to one of six causes:
The first three are data problems. The next two are engineering and operating problems. The last has nothing to do with technology at all. That distinction decides which projects newer models can realistically help.

What Has Changed in Manufacturing Computer Vision-and What Hasn’t

Foundation models pretrained on broad image collections have reduced the labeled data required by certain inspection use cases. Zero-shot and open-vocabulary approaches let teams describe what to look for rather than training a separate model for every defect category from scratch. 
Modern AI defect detection in manufacturing now includes these foundation models, which reduce the labeled data required for industrial inspection across a wider range of part types and defect categories.
Industrial anomaly detection also has a standard reference point. The MVTec Anomaly Detection benchmark, built specifically for industrial inspection, provides defect-free training images for each category and a test set containing both defective and defect-free images, with pixel-precise annotations of the anomalies. It holds more than 5,000 high-resolution images across fifteen object and texture categories. [1] 
That setup mirrors a common plant reality: plenty of good parts, very few bad ones. For manufacturing plants where visual inspection AI programs stalled because defects were rare, anomaly detection methods built around defect-free training images are worth a fresh look.

What has not changed

Better models do not fix optics. Poor lighting, glare, vibration, and inconsistent part positioning still break inspection. Large models can still be too slow for decisions inside a single machine cycle. Integration with manufacturing execution systems (MES) and programmable logic controllers (PLCs) still takes engineering effort. And a project without a clear owner on the plant floor will stall again, whatever model sits underneath.

Six Criteria for Evaluating a Paused Computer Vision Pilot

Use the table below to score each shelved project. It is designed to be completed in a working session with quality, operations, and data teams in the same room.
Criterion Question to ask Signal to revisit Signal to leave shelved
Original blocker Why did the project stop? Data scarcity, variation or labeling cost Business context changed or no owner
Value today Is the machine vision quality control gap still costing money in escapes, scrap or inspector hours? Escapes, scrap or inspector hours persist Line retired or defect designed out
Data on hand Do archived images still exist? Images and some confirmed defects available Nothing retained from the pilot
Speed requirement How fast must a decision happen? Seconds or sampled inspection is acceptable Hard real-time at very high line speed
Integration path Can results reach the line? Clear route to MES, PLC, or operator screen No path, and no budget to build one
Ownership Who will run it in production? Named quality or operations owner Only a data team champion
Score each row as a clear yes, partial, or no. Projects with strong answers on original blocker, value, and ownership are the best candidates, even if the other rows need work.

Sorting projects into three groups

Reopen now

These projects stopped because of data scarcity, part variation, or labeling cost, but still address a live problem and have a named owner. Archived images exist. Speed requirements are manageable. For these, zero-shot inspection or anomaly detection trained on good parts can often be tested within a short, contained assessment.

Reassess with a scoped test

Here the value is real, but one or two rows are uncertain. The line may run fast, or integration may have been the original sticking point. Run a focused test that answers the uncertain question directly, such as whether the model can meet cycle time on the current hardware, before committing to a restart.

Leave on the shelf

Some projects should stay paused. If the line was retired, the defect was designed out, or nobody in operations will own the result, better models change nothing. Closing these formally clears space for the candidates that matter.

A practical reassessment sequence

Deciding when to restart vision AI work is easier with a fixed sequence. The steps below keep the reassessment small and evidence-based.

Common mistakes when reopening a shelved project

Teams that restart vision work too quickly tend to repeat common errors. Watching for them saves a second shelving.

How to Rebuild the AI Visual Inspection Business Case for 2026

Old business cases carry old assumptions. Rebuilding AI inspection ROI for 2026 means checking which inputs have actually moved since the original approval:
One caution: a shelved project that looks attractive only because the new model was tested on easy images has been re-pitched rather than reassessed. Insist on the same difficult cases that stopped it the first time. Manufacturing defect detection AI that clears those, at production line speed and under production lighting, has earned a restart budget. Anything less has earned another test.

How Intuceo Approaches Computer Vision Inspection Reassessments

Reassessments run on the same structure Intuceo uses to judge any AI initiative before it reaches production. The DARWIN AI governance framework separates the question into dimensions that can each be answered independently:
A project can pass on model accuracy and still fail on three of those four, which is why the judgment is never made on a model alone.
For vision work, two capabilities carry most of the delivery. High-fidelity visual inspection applies image segmentation and sub-pixel anomaly detection to sub-millimeter defects, including precision medical optics, where surface anomalies, edge irregularities, and contaminants have to be caught at production speed. Intuceo’s multi-modal vision intelligence capability brings video, image, and metadata streams together so an inspection result lands alongside line system signals instead of a separate console-see how this is applied across our advanced manufacturing AI solutions.
Deployment is half of a reassessment that has to survive audit-a challenge Intuceo addressed directly in its advanced ML inspection pipeline case study. Intuceo delivers in on-premise, private cloud, and air-gapped environments, and client data is not used to train public models. For a plant that cannot accept a hosted model changing behavior between validation runs, that removes the variable rather than managing around it.
PhD-led engineering teams with prior deployments in regulated and high-precision environments deliver solutions to fit your unique needs. See how that applies across our advanced manufacturing AI solutions and to our computer vision and AI capabilities built for it.

Have a vision project sitting on the shelf?

AI Dream Session, Vol. 2: Computer Vision Reimagined is a 45-minute live session with Intuceo on Thursday, September 24, 2026, at 11:00 AM ET. It covers which previously rejected use cases may now be viable, where limitations still hold in production, and the questions worth asking before any project is reopened.
Get the reassessment questions before your next project review

Frequently Asked Questions

A shelved vision project is worth revisiting if it originally failed due to data scarcity, part variation, or labeling cost-not due to line speed limits, integration barriers, or lack of ownership. Start with the reason it stopped. If the blocker was too few defect examples, frequent part variation, or labeling cost, newer vision AI models may help. Then test on archived images from the original pilot, measured against the original acceptance criteria. If the blocker was line speed, integration, or lack of ownership, better models alone are unlikely to change the outcome.

Six criteria determine whether a paused computer vision project is worth restarting in manufacturing:
(1) original blocker,
(2) current cost of the problem, (3) availability of archived images,
(4) line speed requirements,
(5) integration path to MES or PLC, and
(6) named operational ownership. Projects that score well on blocker, value, and ownership are usually the strongest candidates.

Four inputs in an old computer vision inspection business case are worth re-checking in 2026: labeling effort (often lower for foundation model use cases), retraining frequency (potentially less frequent where models generalize across part variants), compute cost per image (potentially higher with larger models at the line), and the value of catching a defect (unchanged-set by your process, not by the model). Re-check the first three against your own parts before any approval, and leave the fourth where the original case had it.

Revisit the ones canceled for data or variation reasons, where the underlying problem still exists, and a plant owner is ready to run the result. Leave closed the projects whose lines were retired, whose defects were designed out, or that lacked operational ownership. A short, documented reassessment is the fastest way to tell the difference.

Why Florida Manufacturers Are Turning to Predictive Maintenance AI

Florida’s manufacturing sector is growing faster than its workforce can keep up. Predictive maintenance AI is helping manufacturers across the state protect production output, reduce unplanned stoppages, and extend the useful life of aging equipment.

Key Takeaways

Florida's Manufacturing Sector: Growth Meets Operational Pressure

Florida’s manufacturing industry contributed $86.6 billion in GDP as of Q3 2025, surpassing both tourism and agriculture in economic output.1 The state now ranks third in the nation for total manufacturing establishments, with over 27,000 facilities employing more than 434,000 workers. [2] Aerospace, defense, medical devices, and electronics are driving much of this expansion.
But growth introduces strain. Florida Commerce Secretary Alex Kelly testified in October 2025 that more than 50% of the state’s manufacturing workforce is 45 years of age or older.[3] When experienced machine operators and maintenance technicians retire, they take decades of institutional knowledge with them. That makes AI-driven approaches to reducing manufacturing downtime a strategic response to a structural workforce challenge.

How Predictive Maintenance AI Works in Manufacturing

Predictive maintenance replaces fixed-schedule servicing with condition-based intervention. Instead of replacing a bearing every 6,000 hours regardless of wear, AI models analyze real-time sensor data, including vibration patterns, temperature fluctuations, acoustic emissions, and electrical current signatures, to determine exactly when that bearing is likely to fail.
The process follows a clear sequence. IoT predictive maintenance sensors collect continuous readings from critical equipment such as motors, compressors, pumps, and conveyor systems. This data flows to an analytics layer where machine learning algorithms establish baselines for normal operating behavior, then flag deviations that match known failure signatures. For example, when the system detects early-stage bearing wear, vibration sensors pick up impulse patterns at frequencies human senses can’t detect, often weeks before any audible symptoms appear.

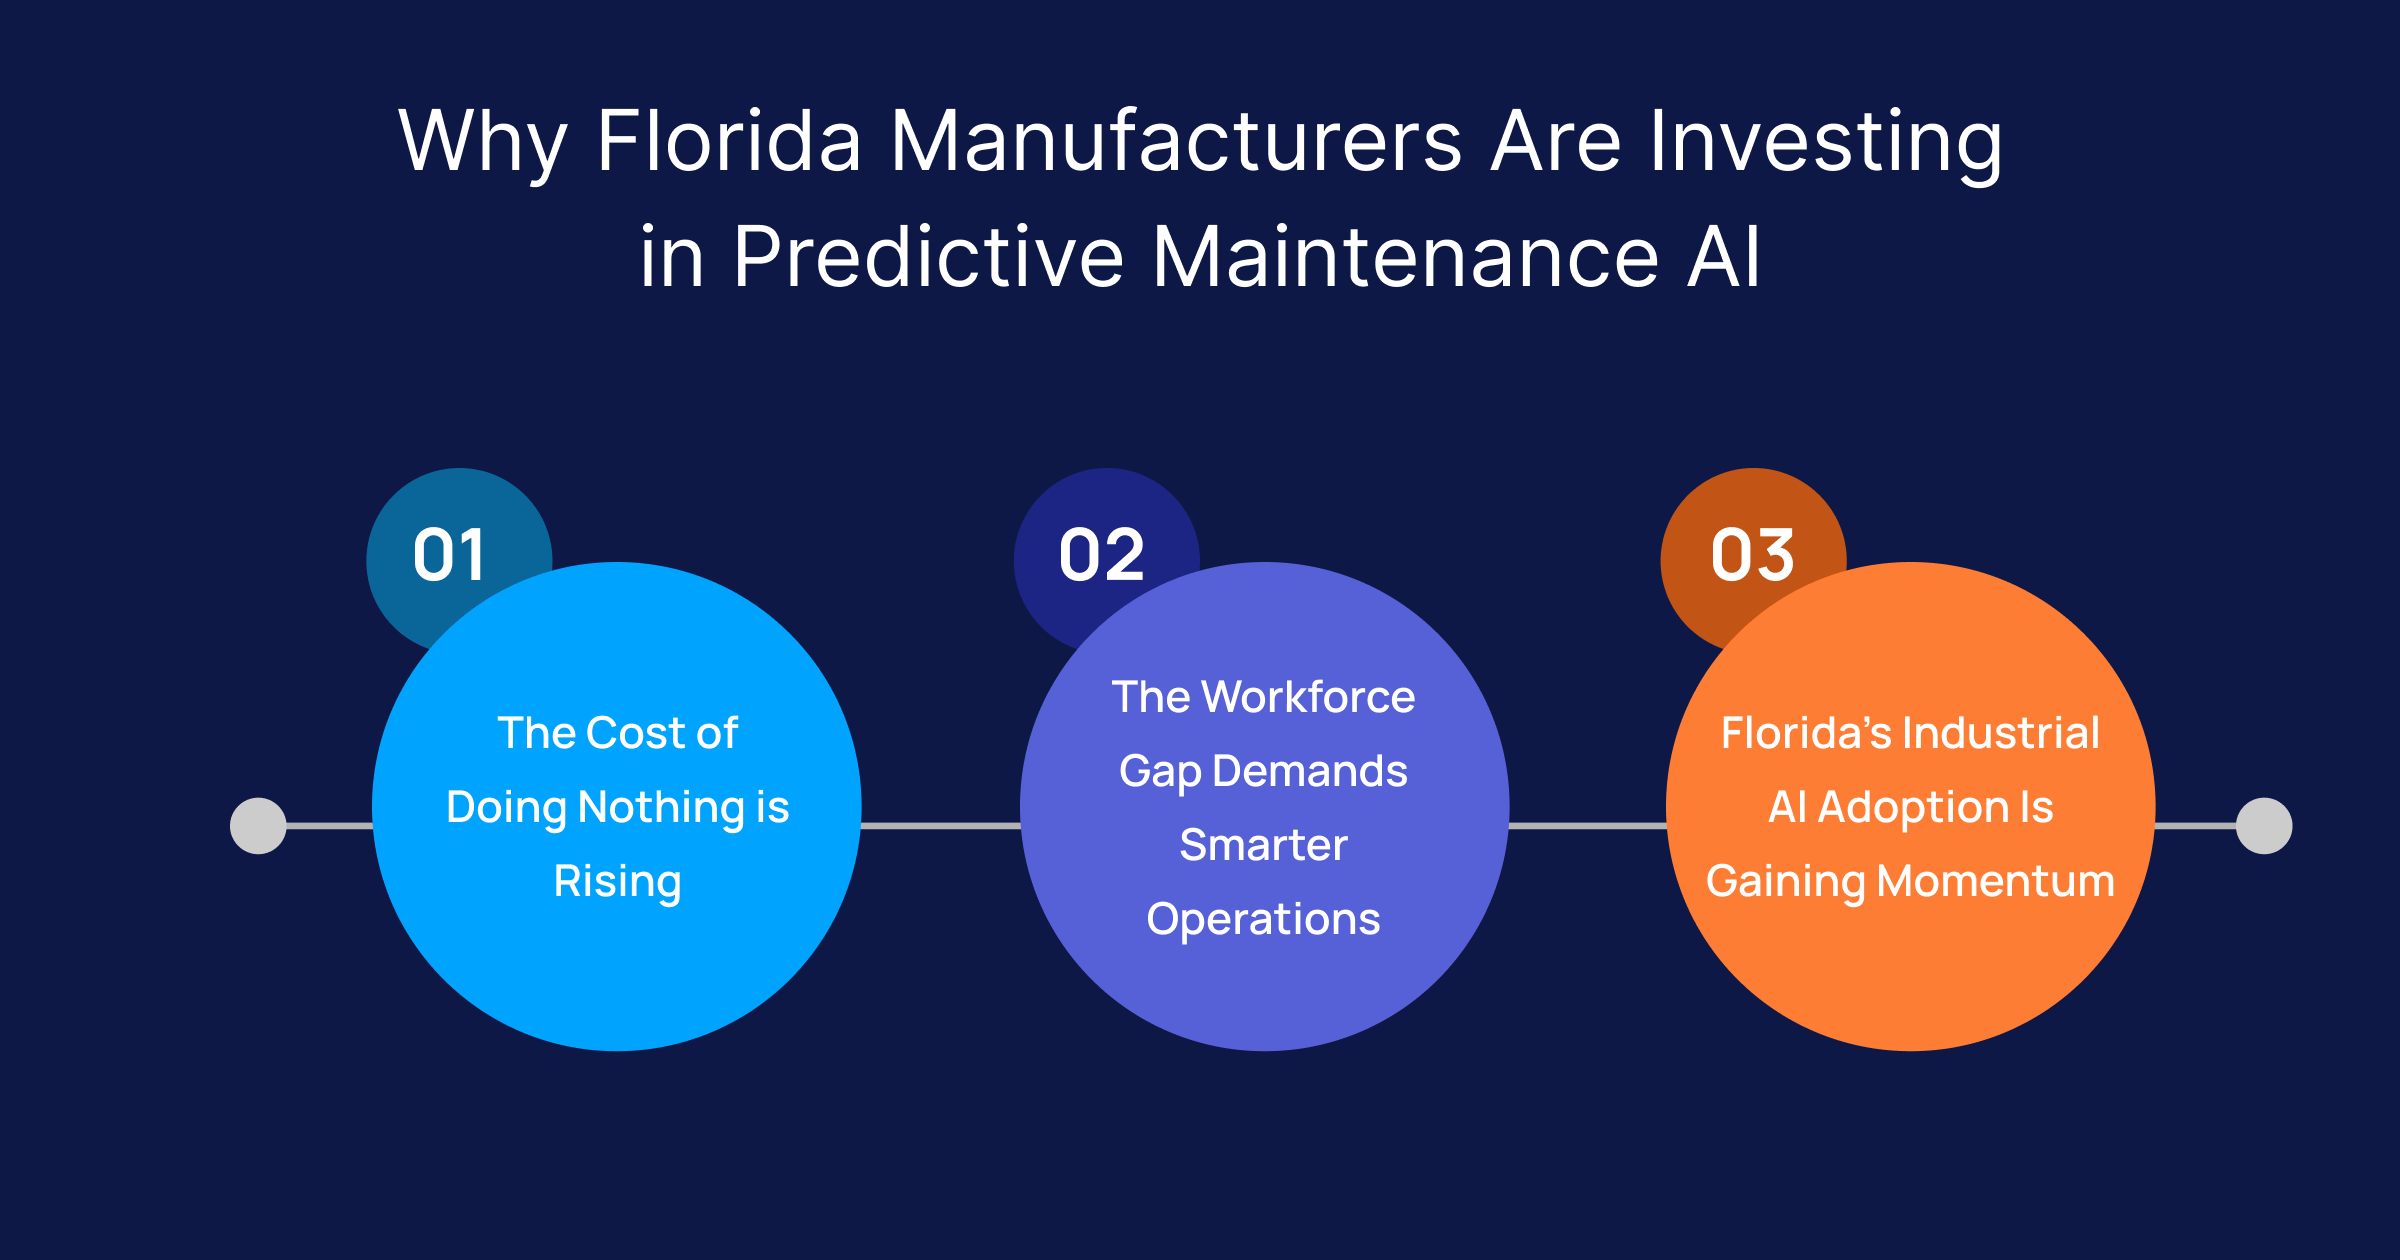
Why Florida Manufacturers Are Investing in Predictive Maintenance AI

Several converging pressures explain why predictive maintenance AI adoption is accelerating across Florida manufacturing operations specifically.

The Cost of Doing Nothing is Rising

Unplanned downtime costs industrial manufacturers an estimated $50 billion annually. [4] And the gap between planned and unplanned repairs is significant: proactive maintenance on the same asset costs four to five times less than an emergency repair after failure.[5] For Florida facilities operating in sectors like aerospace and electronics, where production schedules are tightly contracted, even a single unplanned stoppage can cascade into missed delivery commitments and financial penalties.

The Workforce Gap Demands Smarter Operations

With more than half of Florida’s manufacturing workers approaching retirement,[3] manufacturers cannot rely solely on experienced technicians to diagnose equipment problems by sound and feel. Asset health monitoring powered by AI captures and codifies that diagnostic knowledge, allowing smaller and less experienced maintenance teams to act on data-driven recommendations promptly.

Florida's Industrial AI Adoption Is Gaining Momentum

Florida ranks second in the U.S. for manufacturing job growth, [6] and has seen a 32% increase in manufacturing establishments since 2019.[2] State-backed infrastructure investments, pro-business policies, and a growing concentration of aerospace and electronics production along the Space Coast and Central Florida corridors make the state a natural adoption zone for industrial AI initiatives. Manufacturers expanding into new Florida facilities have the opportunity to build sensor infrastructure from day one, rather than retrofitting legacy plants.

The ROI of Predictive Maintenance AI for Manufacturing Facilities

The financial returns from predictive maintenance in manufacturing are well-documented. McKinsey research indicates that predictive maintenance can reduce equipment downtime by 30% to 50% and lower maintenance costs by 10% to 40%. Most organizations achieve full payback within 12 to 18 months.
Beyond direct cost savings, predictive maintenance AI also extends equipment useful life significantly, allowing facilities to defer major replacements and redirect that capital toward growth.

What Sensors and Data Are Needed for Predictive Maintenance Models?

One of the most common questions from manufacturers evaluating IoT predictive maintenance is what infrastructure investment is required before deployment can begin. The answer is more accessible than many expect.
Four primary sensor types cover the majority of industrial failure modes.
Modern wireless IoT sensors can be retrofitted to existing equipment without modifications, with most installations completed in under an hour per asset. A starting deployment on a facility’s 10 to 15 most critical assets, typically motors, pumps, compressors, and gearboxes, provides enough data to build baseline models and demonstrate value within the first 60 to 90 days. From there, coverage can expand to secondary assets based on failure risk and production impact.

Getting Started: A Practical Roadmap

For Florida manufacturing operations considering predictive maintenance AI, the most effective path forward follows three phases.
The first phase is a targeted pilot. Identify the three to five assets with the highest downtime costs or safety implications. Install vibration and temperature sensors on these assets, establish a two-to-four-week data baseline, and configure initial alert thresholds. This phase typically requires minimal capital and can produce actionable insights within 60 days.
The second phase is validation and expansion. Use the pilot data to calculate actual avoided downtime, quantify savings, and build the internal business case. Expand sensor coverage to the next tier of critical assets and begin integrating AI-generated maintenance recommendations into daily workflows.
The third phase is operational integration. Connect predictive models to your CMMS for automated work order generation, build dashboards for real-time asset health monitoring, and establish continuous improvement loops where model accuracy improves with each confirmed or averted failure.
Working with a team that has prior deployment experience in manufacturing environments can accelerate each of these phases significantly, reducing the typical 90-day pilot to as few as 30 to 45 days and avoiding common pitfalls around sensor placement, data integration, and false-positive tuning.

Stop Unplanned Downtime Before It Starts.

Leverage AI-driven insights to predict equipment failures, cut maintenance costs, and maximize production output across your Florida facility.

Frequently Asked Questions

Preventive maintenance follows a fixed schedule, servicing equipment at set intervals regardless of actual condition. Predictive maintenance uses real-time sensor data and AI algorithms to monitor equipment health continuously, triggering intervention only when data indicates early signs of degradation. This prevents both unnecessary servicing of healthy assets and the costly surprise of an unplanned breakdown. Where preventive maintenance asks “Is it time?”, predictive maintenance asks “Is it needed?”
Manufacturers need IoT sensors (vibration, temperature, pressure, or current) installed on critical assets, a reliable network for data transmission, and a system to store and process the data. Most modern wireless sensors can be retrofitted to existing equipment without modifications. A baseline of two to four weeks of normal operating data is typically required before AI models can begin generating accurate failure predictions.
McKinsey research indicates that manufacturers implementing predictive maintenance AI can expect a 30% to 50% reduction in unplanned downtime. Individual outcomes depend on equipment age, the number of monitored failure modes, and how consistently maintenance teams act on the alerts. Organizations that integrate automated work order generation tend to see results at the higher end of that range.
Predictive maintenance in manufacturing delivers the strongest returns in industries with capital-intensive rotating equipment and high downtime costs. Aerospace and defense, food and beverage, automotive, pharmaceuticals, and energy and utilities are among the leading adopters. Within Florida specifically, the concentration of aerospace manufacturing along the Space Coast and electronics production in Central Florida makes these sectors natural candidates for early adoption.